Primary target long-tail keyword: induction foil seal testing for oral pouch cans OEM packaging
An induction membrane can add tamper evidence and barrier protection, but only when the foil, heat-seal layer, can resin, rim and cap pressure work together. A shiny disk attached to the opening is not proof of a reliable seal. Channels, scorched liners and partial bonds often hide under an apparently complete surface.
Oral pouch packs add practical complications. Flavor vapor can reach the rim, powder can sit on the land area, and a tall stack of pouches may prevent the cap from applying even pressure. Validation must use the filled commercial can at normal line speed.
Confirm why the foil is needed
Define whether the membrane provides tamper evidence, moisture barrier, aroma retention, leak control or a combination. The function determines material and acceptance criteria.
If consumers expect a peelable opening, opening force and clean removal matter. A permanent weld that tears into fragments may protect the product and still create a poor experience.
Match the seal layer to the can resin
Polypropylene, polyethylene and other container materials need compatible heat-seal layers. Similar-looking liners may bond at different energy settings or fail after storage.
Lock liner supplier, construction and resin. A purchasing substitution requires testing; “same diameter” is not an equivalence statement.
Inspect the sealing land
The can rim must be flat, clean and dimensionally consistent. Mold flash, ovality and dents create local gaps. Flavor oil or powder on the rim blocks contact.
Add a controlled pre-seal inspection and keep filling below the rim. Increasing induction power will not repair contaminated or distorted containers.
Control cap application first
The closure holds the liner against the rim while it passes under the induction head. Uneven or low application torque produces weak sectors even when energy is correct.
Measure cap application and removal behavior with the intended liner stack. Foam backing, pulp board and one-piece liners distribute pressure differently.
Develop an operating window
Challenge line speed, head height and power around the center setting. Too little energy leaves partial adhesion. Too much can wrinkle foil, distort the rim, discolor the backing or make the seal brittle.
Run cold startup, steady operation and restart conditions. Equipment warm-up and conveyor gaps can shift the delivered energy.
Use several inspection methods
Visual inspection should cover full circumference, wrinkles, scorching and channels. Peel or removal-force testing adds a measurable trend when the package is designed to peel.
Leak or vacuum methods can challenge integrity, but the method must fit a porous product and vented or nonvented package design. Define sample preparation and failure criteria.
Check after conditioning
Test freshly sealed cans and samples held long enough for the bond to stabilize. Then add heat, humidity, vibration and drop conditions representative of distribution.
A seal may pass immediately and lift after flavor vapor, rim stress or plastic relaxation acts during storage. Retained samples help separate liner failure from closure damage.
Protect the pouch sensory profile
Induction heat should not noticeably damage top-note flavor or deform pouches near the lid. Excess head energy and slow speed can warm the package more than expected.
Compare headspace odor and sensory performance with an unsealed control during development. Barrier improvement should not introduce a burnt liner note.
Write the OEM packaging specification
- Can resin and rim dimensions
- Liner construction
- Cap application range
- Head height
- Power and speed window
- Visual criteria
- Peel or leak method
- Sampling frequency
- Restart rule
- Change-control triggers
Keep the settings and results with the packaging record. When one market reports lifted seals, the factory can review actual can, liner and line lots instead of guessing.
Questions Buyers Usually Ask
Does every oral pouch can need an induction foil seal?
No. The decision depends on tamper-evidence needs, barrier target, route, closure design and market expectations.
Can induction power be increased to fix weak seals?
Only after confirming rim cleanliness, liner compatibility, cap pressure and head alignment. Excess power can create a different failure.
Provide the can resin, rim drawing, closure, liner proposal and shipping route for an induction-seal trial plan before printed components are purchased.
Recommended Blog Images
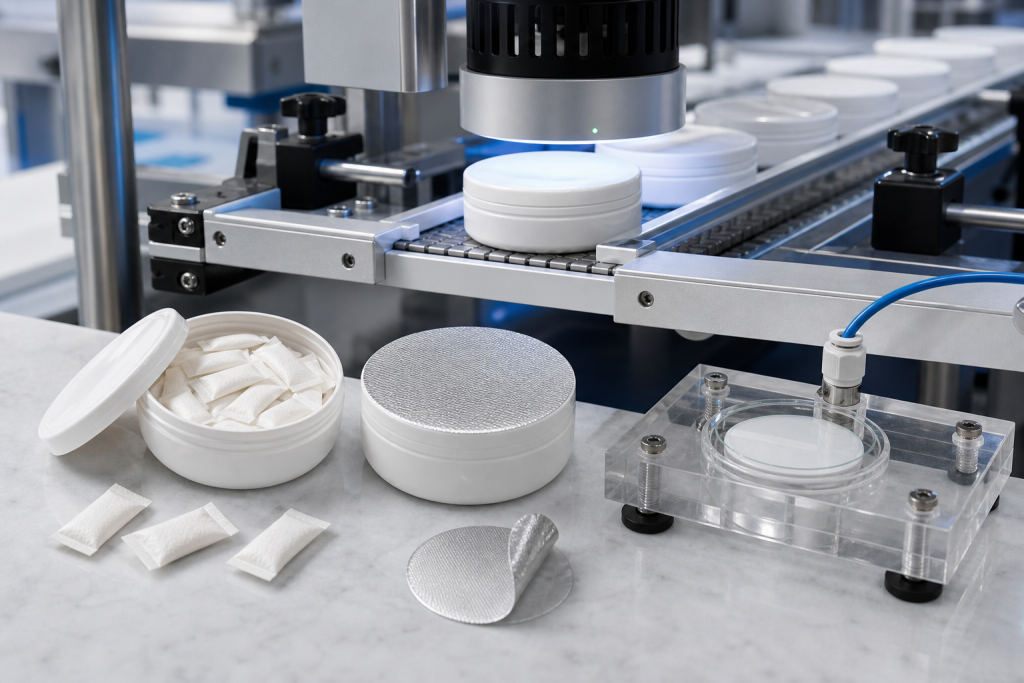
- Packaging-line photograph with realistic pouches, unbranded cans, foil membranes and induction head.
- Seal-window graphic covering cap pressure, head height, power, speed and inspection results.
Sample around line interruptions
Steady production is usually the easiest condition. Collect cans at startup, after conveyor jams, after cap or liner replenishment and following head-height adjustment. A can that pauses under the induction head can overheat, while one spaced too closely after restart may receive insufficient energy. The restart procedure should state which cans are isolated and retested.
Separate liner and closure complaints
A lifted foil does not always mean poor induction energy. Cap cocking, damaged threads and inconsistent liner insertion can reduce contact before heating. Mark the weak sector and compare it with cap position, rim dimensions and liner placement. This avoids increasing power until good cans scorch while the mechanical fault remains.
Verify consumer opening after storage
Measure peel behavior after normal and stressed storage, not only minutes after sealing. Adhesion can strengthen, weaken or become uneven as plastic relaxes and flavor vapor reaches the interface. Inspect for foil fragments and sharp edges. Barrier performance is valuable only when the user can remove the membrane cleanly without tools or product contamination.
Confirm foil diameter and centering at normal feeder speed. An off-center membrane can appear bonded across most of the rim while leaving one narrow channel that opens during vibration or warm storage.
Related manufacturing references
For a complete OEM review, connect this article with the main product and process pages. Buyers usually need category fit, stock-formula options, custom formulation support, process checks, and a direct project discussion before approving samples.
- Custom oral pouch manufacturing
- Stock formulation options
- Private label pouch project planning
- Formulation and R&D support
- Manufacturing process and quality checks
- Technical manufacturing blog
- Discuss a project
Content review note: technical articles are reviewed for functional oral pouch, ODF, packaging, and OEM procurement relevance.