Primary target long-tail keyword: metal detection for functional oral pouch manufacturing
Installing a metal detector does not automatically create a controlled process. Mineral-heavy formulas can behave differently from dry cellulose blends, foil-lidded cans cannot pass through every detector arrangement, and a test piece placed on top of a can may be easier to find than contamination buried between moist pouches.
The useful discussion starts with the hazard analysis. Identify where metal could enter, decide the last practical detection point, establish achievable sensitivity for the actual product and package, then challenge the system during production.
Map credible sources of metal
Review sieves, mixer blades, fasteners, pumps, cutters, sealing jaws and conveyors. Maintenance activity can introduce wire, drill swarf or missing hardware after the line was previously qualified.
Incoming botanical powders may contain field or processing fragments. Supplier controls, magnets and screening can reduce risk before the material reaches sensitive filling equipment.
Choose the inspection point carefully
Detection should occur after the last step reasonably likely to introduce metal, when feasible. For pouch production that may be after cutting and sealing but before cans receive foil or metalized components.
If finished packaging interferes with detection, document the alternative controls and line position. Do not move the detector upstream without reconsidering hazards created later.
Understand product effect
Moisture, salt, minerals and temperature can create signals that resemble metal. Semi-moist electrolyte or zinc formulas may require different settings from a dry caffeine pouch.
Validate each product family at normal and worst-case conditions. One sensitivity claim from an empty conveyor is not evidence for every SKU.
Use traceable challenge pieces
Ferrous, non-ferrous and stainless-steel test pieces usually behave differently. Define sizes from risk assessment and demonstrated equipment capability instead of selecting the smallest catalog set for appearance.
Keep pieces controlled, identified and reconciled. A missing test wand is itself a foreign-body incident that requires immediate line action.
Place tests through the difficult position
Pass challenge pieces with representative product and at positions most difficult for the aperture to detect. Rotate location among front, center and rear or the validated worst point.
Test at operating speed and with typical can spacing. Hand-carrying a sample slowly through the center may produce an easy pass that the commercial line cannot repeat.
Verify rejection, not only detection
Confirm the reject device removes the correct unit into a secured container and that line backup does not push it back into acceptable product. Challenge alarms, stop functions and bin-full controls where fitted.
Reconcile rejected units and test pieces. An alarm without physical segregation leaves quality dependent on operator memory.
Respond to a failed challenge
Stop the line, isolate product since the last successful check, correct the equipment and repeat the challenge. The disposition plan should be written before a failure occurs.
Simply passing the test a second time does not explain the first failure. Check settings, aperture contamination, electrical interference, belt tracking and product conditions.
Pair detection with prevention
Inspect equipment for wear, count critical parts and control maintenance tools. Metal detection is one layer, not permission to operate damaged machinery.
Trend findings and false rejects. Repeated nuisance alarms can cause operators to weaken settings, while repeated fragments point to an upstream failure that needs correction.
Write buyer-ready evidence
- Hazard assessment
- Detector location
- Validated product groups
- Test-piece materials and sizes
- Worst-case position
- Check frequency
- Reject verification
- Failure hold boundary
- Calibration and service records
Ask for records from the actual line and SKU. A brochure sensitivity measured under ideal conditions should not become the finished-product guarantee.
Questions Buyers Usually Ask
Can finished foil-sealed cans go through a metal detector?
Sometimes packaging and product effect make conventional detection impractical. The manufacturer must evaluate the real configuration and choose a justified control point.
Does metal detection find glass or hard plastic?
No. Other foreign-material controls, and sometimes X-ray or optical systems, are needed according to the hazard assessment.
Share the formula minerals, pouch size, can components and proposed line route so foreign-body controls can be reviewed before commercial packaging is ordered.
Recommended Blog Images
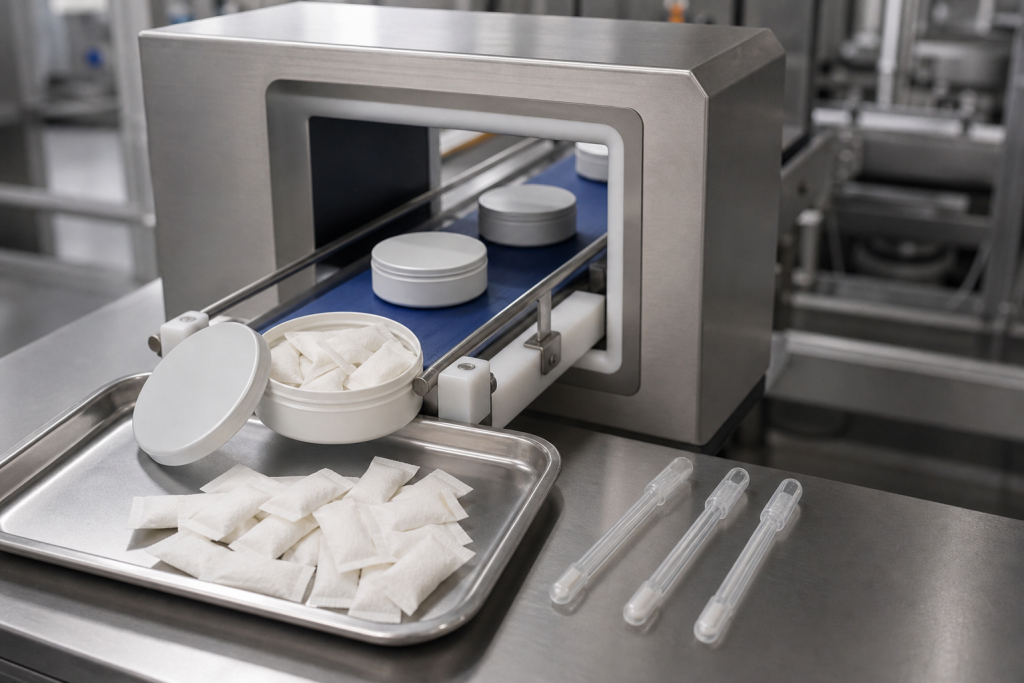
- Packaging-line photograph showing unbranded cans, realistic pouches and a compact metal detector.
- Hazard-control flow from incoming screening and equipment inspection to final challenge checks.
Challenge the detector after product changes
A setting qualified for a dry mint pouch should not be carried automatically to an electrolyte, zinc or semi-moist formula. Product conductivity, temperature, pouch count and orientation can change the detector signal. Run a documented challenge when a new SKU enters the validated product group and confirm that sensitivity remains reliable without excessive false rejects.
Control the boundary around maintenance
Maintenance work creates an unusual concentration of foreign-body risk. Count tools and replaced parts, inspect the product zone, clean the line and repeat the detector challenge before release. If a screw, wire fragment or blade section is missing, isolate material back to the last verified condition. A signed work order alone does not prove the line is clear.
Review rejects instead of discarding them silently
Open rejected cans under controlled conditions and determine whether the signal came from metal, product effect or packaging. Record the location and type of any fragment. Several similar findings can identify a failing screen, worn cutter or loose fastener. A growing false-reject rate is also useful: it can show environmental interference or a drifting product condition before operators reduce sensitivity.
Challenge records should identify the operator, time, product, line speed and result. This makes the control auditable and shows whether failures cluster around one shift, setting or formula family.
Related manufacturing references
For a complete OEM review, connect this article with the main product and process pages. Buyers usually need category fit, stock-formula options, custom formulation support, process checks, and a direct project discussion before approving samples.
- Custom oral pouch manufacturing
- Stock formulation options
- Private label pouch project planning
- Formulation and R&D support
- Manufacturing process and quality checks
- Technical manufacturing blog
- Discuss a project
Content review note: technical articles are reviewed for functional oral pouch, ODF, packaging, and OEM procurement relevance.